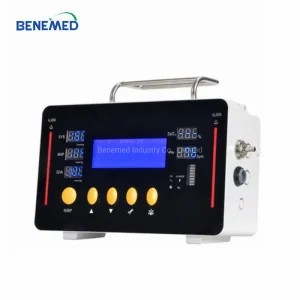
Explore our high-performance diagnostic and clinical support systems engineered for elite healthcare facilities worldwide.
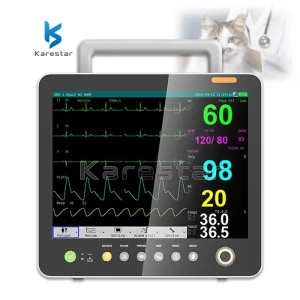
Guangzhou Medivara Medical Co., Ltd. is a leading China manufacturer of medical beds, ICU equipment, and adjustable hospital furniture, dedicated to enhancing patient comfort, safety, and clinical efficiency. With years of experience in the healthcare equipment industry, Medivara has become a trusted partner for hospitals, clinics, and medical facilities worldwide.
The company specializes in producing a comprehensive range of healthcare furniture and equipment, including electric and manual medical beds, ICU beds, pediatric and birthing beds, overbed tables, hospital chairs, medical cabinets, wheelchairs, crash carts, and patient monitoring systems. Each product is designed with ergonomics, durability, and hygiene in mind, ensuring both patients and healthcare professionals benefit from high-quality, reliable equipment.
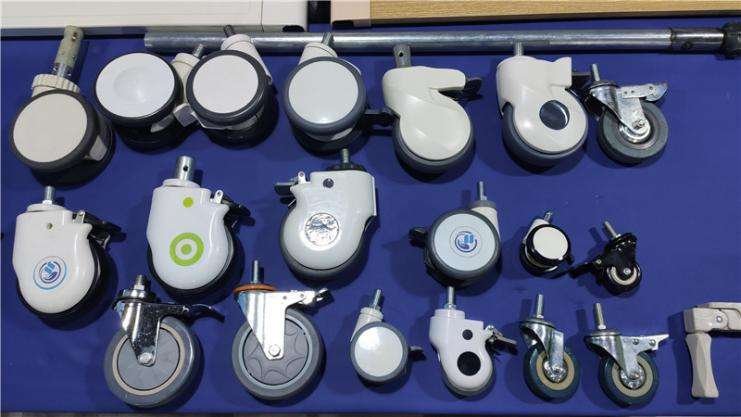
Medivara places a strong emphasis on innovation and safety, integrating advanced materials, intelligent adjustment systems, and hospital-grade designs into its furniture and equipment. The company maintains strict quality control standards and adheres to international healthcare certifications, ensuring every product meets or exceeds global medical requirements.
With a professional R&D team, modern production facilities, and a dedicated after-sales support network, Guangzhou Medivara Medical Co., Ltd. provides customized OEM solutions, timely delivery, and comprehensive guidance for healthcare projects.
Committed to excellence, innovation, and customer satisfaction, Medivara Medical continues to advance the hospital furniture industry, delivering high-performance, safe, and patient-centered solutions that enhance healthcare operations across China and the world.
The global cardiology equipment and intensive care furniture landscape is undergoing a massive transformation driven by an aging global population, rising prevalence of cardiovascular diseases, and the rapid digitization of hospital infrastructure. Modern medical procurement managers are no longer looking for isolated pieces of hardware; instead, they require integrated ward ecosystems where patient monitors, smart hospital beds, and emergency crash carts communicate seamlessly.
Key procurement priorities for international healthcare institutions include IoT-enabled vital sign monitoring, ergonomic patient transfer solutions to minimize nurse injury risks, and antimicrobial surface finishes that reduce hospital-acquired infections (HAIs). As a premier Chinese manufacturer, Medivara aligns its production scaling directly with these macro-level clinical demands, providing modular infrastructure upgrades that satisfy both tertiary hospitals and rural community clinics.
Our ongoing engineering roadmap focuses on AI-driven diagnostic assistance integration, automated position adjustments based on real-time patient pressure mapping, and energy-efficient battery backup systems for emergency transport equipment. By partnering closely with clinical researchers, Medivara anticipates future regulatory shifts and ergonomic requirements, ensuring that every manufactured unit—from electric hospital beds to advanced patient monitors—remains at the cutting edge of medical technology.
Furthermore, our macro-level hospital turnkey solutions provide comprehensive blueprinting for new healthcare facilities. We combine spatial layout optimization with high-durability medical furniture provisioning, significantly reducing deployment friction for government health ministries and private hospital groups.
Discover our full spectrum of specialized medical devices, emergency crash carts, and patient transfer trolleys designed for optimal clinical workflow.
Navigating international regulatory frameworks is critical for medical device procurement. Medivara operates under strict quality management systems compliant with ISO 13485, CE, and FDA standards. Our regulatory documentation team assists international distributors and hospital procurement officers with full dossier support, ensuring seamless customs clearance and regional registration.
Beyond manufacturing excellence, we provide dedicated localization support, including multi-language user manuals, technical training webinars, and local spare parts warehousing. This robust after-sales commitment ensures maximum uptime for mission-critical cardiology and ICU departments across more than 120 countries.
Expert answers to common queries regarding our manufacturing capabilities, compliance standards, and global procurement processes.
Our entire product line is manufactured in strict accordance with ISO 13485 quality management standards. Most of our medical beds, patient monitors, and emergency crash carts also feature CE and FDA compliance certifications, meeting rigorous international safety and efficacy benchmarks.
Yes, we specialize in comprehensive OEM and ODM partnerships. Our in-house R&D engineering team collaborates closely with global clients to tailor dimensions, electrical specifications, branding, and specialized clinical features to match specific hospital tender requirements.
Standard production lead times typically range from 20 to 35 days, depending on the order volume and customization complexity. For large-scale hospital turnkey projects, our project management team establishes a phased delivery schedule aligned with your site preparation milestones.
We maintain a dedicated global after-sales support network offering remote technical troubleshooting, comprehensive video installation guides, warranty replacement parts, and localized distributor training programs to guarantee uninterrupted clinical operations.
 Medivara Medical